Exporting glass-processing machinery since 2002, with international project support from planning to installation and training.


Automatic Insulating Glass Production Line – SKIL-A Series
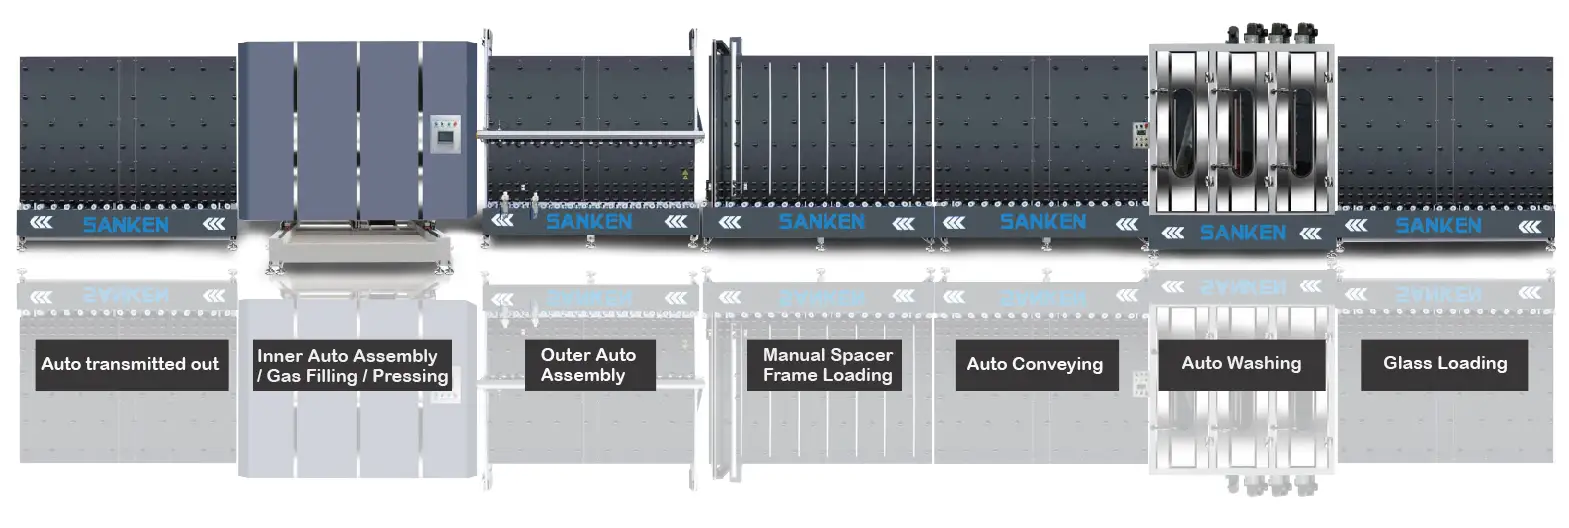
The SANKEN SKIL-A series connects glass washing and drying, manual spacer frame loading, automatic assembly, inert-gas filling, pressing and discharge in one main insulating glass line. PLC and touch-screen control coordinate the processing stages, while coating-side identification supports Low-E glass handling.
- Models: SKIL-2000A and SKIL-2500A.
- Maximum IGU size: 2000 × 3000 mm or 2500 × 3500 mm.
- Individual glass thickness: 3–12 mm.
- Spacer thickness: 6–27 mm.
- Total IGU thickness: 10–56 mm.
- Conveying speed: 0–45 m/min.
- Production efficiency with gas filling: 60–80 units/hour, depending on unit specifications and process settings.
- Line expansion: Connect glass loading, Low-E coating deletion and secondary sealing equipment according to production requirements.
Automatic Insulating Glass Production Line
SANKEN SKIL-A series combines vertical glass washing and drying, spacer frame positioning, automatic assembly, online inert-gas filling, pressing and discharge in one main insulating glass line. PLC and touch-screen control coordinate the processing sections for double- and triple-glazed insulating glass production.
Choose SKIL-2000A for IGUs up to 2000 × 3000 mm or SKIL-2500A for IGUs up to 2500 × 3500 mm. Both models process individual glass panes 3–12 mm thick, spacers 6–27 mm thick and finished IGUs with a total thickness of 10–56 mm, subject to the selected glass and spacer combination.
Spacer frames are loaded manually. Automatic glass loaders, Low-E coating deletion equipment and secondary sealing systems can be connected according to the production arrangement.
Production Line Views
Main Features
PLC and Touch-Screen Control
Operators use the touch-screen interface to control the main line and adjust operating settings. Centralized PLC control coordinates washing, conveying, assembly, gas filling and pressing.
Adjustable Conveying Speed
Frequency-controlled conveying provides a speed range of 0–45 m/min. Adjust the conveying speed to match glass dimensions and the requirements of each processing stage.
Vertical Washing and Air-Knife Drying
The washing section uses stainless steel and corrosion-resistant materials, three pairs of brushes and two sets of high-pressure air knives. Washing removes surface contamination, while air-knife drying prepares the panes for spacer placement and assembly.
Low-E Coating-Side Identification
Automatic coating-side identification supports the correct orientation of Low-E glass during washing and assembly. Review the coating type and washing requirements when configuring the line.
Automatic Assembly and Glass Size Detection
The line includes external and internal automatic assembly sections. The pressing section detects glass length and height to coordinate assembly and pressing for different panel sizes.
Online Inert-Gas Filling
The integrated filling section introduces inert gas during the assembly process for double- and triple-glazed IGUs. Select the gas supply and filling settings for the intended unit structure and production requirements.
Automatic Pressing and Discharge
After assembly and gas filling, the unit is pressed and conveyed out of the main line for the next operation. A compatible secondary sealing system can be connected downstream.
Production Process
Glass Loading → Vertical Washing & Drying → Conveying → Manual Spacer Frame Loading → Automatic Assembly → Inert-Gas Filling & Pressing → Discharge
1. Glass Loading and Washing
Feed prepared glass panes into the vertical washing section. For glass that requires Low-E edge deletion, complete that operation before washing or connect an upstream coating deletion machine.
2. Spacer Frame Preparation and Positioning
Prepare the spacer frame, desiccant and primary butyl seal with the appropriate auxiliary equipment. The operator positions the prepared frame at the manual spacer loading station.
3. Assembly, Gas Filling and Pressing
The line assembles the glass panes and spacer frame, fills the cavity with inert gas and presses the unit. Set the process for the required double- or triple-glazed construction.
4. Discharge and Secondary Sealing
The assembled unit leaves the main line for secondary sealing and subsequent handling. Select a sealing robot or a sealant extruder and sealing table to match the production plan.
Technical Specifications
| Parameter | SKIL-2000A | SKIL-2500A |
|---|---|---|
| Max. IGU Size | 2000 × 3000 mm | 2500 × 3500 mm |
| Min. IGU Size | 300 × 400 mm | 300 × 400 mm |
| Individual Glass Thickness | 3–12 mm | 3–12 mm |
| Spacer Thickness | 6–27 mm | 6–27 mm |
| Total IGU Thickness | 10–56 mm | 10–56 mm |
| Conveying Speed | 0–45 m/min | 0–45 m/min |
| Production Efficiency with Gas Filling | 60–80 units/hour | 60–80 units/hour |
| Air Pressure | 0.7–0.8 MPa | 0.7–0.8 MPa |
| Total Power | 34.6 kW | 38.6 kW |
| Line Dimensions (L × W × H) | 21500 × 2800 × 2950 mm | 24500 × 2800 × 3450 mm |
| Machine Weight | 7100 kg | 9000 kg |
The conveying speed is the transport speed of the line. Production efficiency with gas filling is 60–80 units/hour; actual output varies with glass size, IGU structure, gas-filling settings and handling time. Line dimensions and power figures apply to the main SKIL-A line. Additional equipment requires separate space and utilities.
Double, Triple and Low-E Insulating Glass
Double-Glazed Units
The line assembles two glass panes around a prepared spacer frame, with online inert-gas filling and pressing before secondary sealing.
Triple-Glazed Units
The assembly and filling process also supports triple-glazed units. Confirm the full glass-and-spacer build-up so that individual pane thickness, spacer thickness and total unit thickness remain within the machine limits.
Low-E Glass Units
Coating-side identification and a washing section configured for Low-E glass support coated-glass processing. Where the selected coating requires edge deletion for sealing, connect the appropriate upstream equipment.
IGUs produced with the line can be used for windows, doors, facades and other architectural glazing. Thermal, acoustic and durability performance depends on the complete IGU design, materials and manufacturing process.
Equipment for an Extended IG Production Line
Build the production arrangement around the main SKIL-A line and add equipment for the operations your factory requires.
- Automatic glass loading and unloading equipment for material handling.
- Low-E coating deletion equipment for edge preparation before washing.
- Spacer bending or preparation equipment for the selected spacer system.
- Desiccant filling equipment and a butyl extruder for spacer frame preparation.
- An automatic two-component sealing robot, or a sealant extruder with a sealing table, for secondary sealing.
Confirm the equipment list, processing direction and utility requirements together when planning the complete line.
Factory Layout and Installation Planning
Arrange incoming glass, spacer preparation, the main line, secondary sealing and finished-unit handling in a connected production flow. Allow access for glass movement, maintenance and service connections along the vertical line.
The SKIL-2000A main line measures 21500 × 2800 × 2950 mm, and the SKIL-2500A main line measures 24500 × 2800 × 3450 mm. These equipment dimensions do not include all working aisles, storage positions or auxiliary machines.
Plan compressed air at 0.7–0.8 MPa, the electrical supply, washing-water connections and the inert-gas supply. Coordinate upstream coating deletion and downstream sealing equipment with the selected glass sizes and production direction.
The SKIL-2500A layout example combines the main insulating glass line with secondary sealing and spacer preparation equipment. Its overall arrangement is approximately 34907 × 6762 mm. This extended arrangement has a different footprint from the main line alone; we adapt the layout to your factory dimensions and equipment selection.
Frequently Asked Questions
Which models are available?
The SKIL-A series includes SKIL-2000A and SKIL-2500A, with maximum IGU sizes of 2000 × 3000 mm and 2500 × 3500 mm respectively.
Is spacer frame loading automatic?
Spacer frames are loaded manually at the frame positioning station. The main line automates washing, conveying, assembly, gas filling, pressing and discharge.
Can the line make triple-glazed units?
Yes. The assembly and gas-filling system supports double- and triple-glazed units. Confirm the proposed glass and spacer combination against the individual pane, spacer and total IGU thickness limits.
Does the main line include secondary sealing?
Secondary sealing uses a separate connected sealing robot or sealant extrusion system. Include the required sealing equipment when specifying the production arrangement.
Is 45 m/min the production output?
No. It is the maximum conveying speed. The production efficiency with gas filling is 60–80 units/hour, with actual output depending on unit dimensions, structure and process settings.
What should I send for model selection?
Send your maximum and minimum glass sizes, individual pane thicknesses, double- or triple-glazed unit structure, spacer type and dimensions, Low-E requirements, target output, factory drawing and available utilities.
Plan Your Insulating Glass Production
SANKEN has been exporting glass-processing machinery since 2002. Send us your IGU specifications and workshop drawing to discuss the SKIL-A model, auxiliary equipment and line arrangement.
Contact SANKEN for model selection and a production-line quotation.
SANKEN Glass Machinery is a Guangzhou-based manufacturer and international supplier of glass-processing machinery and complete production-line solutions.
Contact Us
Contact: Dalia Qiu
Tel: +86 15994813914
Landline: +86-20-82347228
Email: sales@sankenglass.com
WhatsApp: +86 15994813914
ADD: No.2, Xinghai Road, Lanhe, Nansha District, Guangzhou City, China. P.C 511480